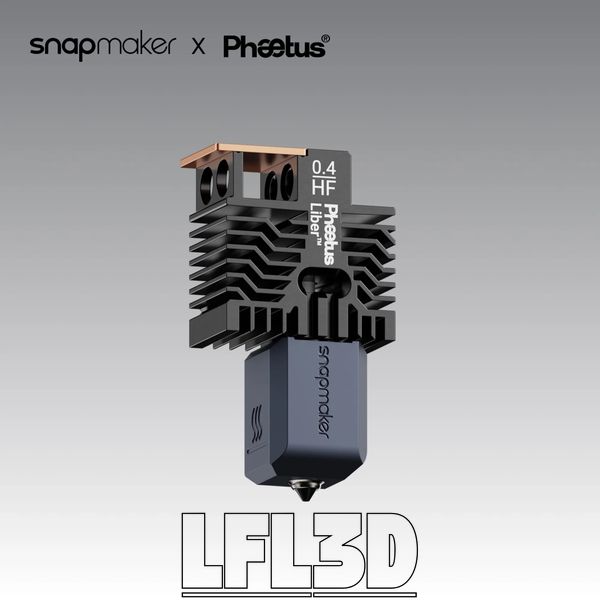
Phaetus Liber™ High Flow Hotend for Snapmaker U1 is a high-performance hotend assembly featuring a 0.4 mm hardened steel nozzle with a DLC coating. Jointly developed by Snapmaker and Phaetus, it incorporates Liber™ Split-Flow technology for more efficient filament melting and delivers a maximum claimed volumetric flow rate of 55 mm³/s. It is designed to accelerate the printing of large models with long, continuous extrusion paths while maintaining consistent material flow.
Liber™ was developed by Phaetus and is manufactured by Runice Co., Ltd. The FlowCore™ marking identifies products manufactured under license in accordance with the patents published at flowcoreip.com.
Key Advantages
Liber™ Split-Flow
Optimized melt channel geometry improves heat transfer to the filament and supports high volumetric flow rates without increasing power consumption.
DLC-Coated Nozzle
Hardened steel combined with a diamond-like carbon coating improves surface hardness and nozzle wear resistance.
Titanium Alloy Heat Break
A seamless heat break with a precisely finished internal surface of Ra ≤ 0.2 μm helps reduce material buildup and the risk of clogging.
High-Flow Printing Performance
55 mm³/s
Maximum Flow Rate
Maximum value claimed by the manufacturer.
Up to +87%
Higher Volumetric Flow
Compared with the standard hotend under the manufacturer's test conditions.
Up to −51.98%
Printing Time
Reduced printing time for a large test model: from 7 h 59 min to 3 h 50 min.
Important: Test Results
The reported improvements in flow rate and printing time were obtained during manufacturer testing. Actual performance depends on the filament, model geometry, temperature, acceleration, slicing parameters, and other printing conditions. The greatest benefits are typically achieved when printing large models with long, continuous extrusion paths. Parts with numerous corners and frequent changes in direction may show smaller improvements.
Liber™ Split-Flow Technology
Thanks to its specially engineered melt channel geometry, Liber™ Split-Flow provides more efficient heat transfer to the filament. The material can melt more uniformly even at higher feed rates, helping to reduce the risk of under-extrusion and maintain the quality of printed parts.
Faster Melting
Optimized contact between the material and heated zone for efficient extrusion.
Consistent Material Flow
Improved melting helps maintain the required material flow along long, high-speed extrusion paths.
Surface Quality
Consistent extrusion contributes to uniform layers, well-formed bridges, and fine details.
Wear-Resistant Nozzle and Clog Prevention
The hotend features a 0.4 mm hardened steel nozzle with a DLC coating. According to Phaetus, the coating has a surface hardness of approximately HV 2000, while the underlying steel has a hardness of HV 725–780. These values refer to different layers of the construction and should not be interpreted as the overall hardness of the nozzle. Precision finishing of the seamless titanium alloy heat break provides a typical internal surface roughness of Ra ≤ 0.2 μm, helping to limit filament residue buildup.
Compatible Materials and Usage Considerations
Liber™ High Flow Hotend supports a wide range of filaments, including PLA, PETG, ABS, ASA, PA, PC, PVA, and support materials, provided that the printer settings meet the requirements of the specific material. The maximum hotend temperature is 300 °C.
High-Flow Mode Limitations
The manufacturer does not recommend high-flow printing with carbon-fiber- or glass-fiber-filled filaments (CF/GF), wood-filled materials, or TPU. Filled materials may cause clogging, while flexible filaments can lead to inconsistent feeding. A suitable standard hotend is generally a better choice for these applications.
When switching from high-temperature materials such as ABS, ASA, PA, or PC to PLA or PETG, Snapmaker recommends cleaning the filament path using the cold pull method according to its official instructions.
Installation on Snapmaker U1
The hotend is designed for the Snapmaker U1 and comes preassembled with a thermistor. High-Flow operation requires firmware V2.0.0 or later. After installation, select the High-Flow hotend type and 0.4 mm nozzle diameter in the printer settings, then perform toolhead offset calibration, bed leveling, and dynamic flow calibration. All nozzles used within the same print job must have the same diameter.
Technical Specifications
| Parameter |
Value |
| Model |
Phaetus Liber™ High Flow Hotend for Snapmaker U1 |
| Compatibility |
Snapmaker U1 |
| Nozzle Diameter |
0.4 mm |
| Nozzle Material |
DLC-coated hardened steel |
| Melting Technology |
Liber™ Split-Flow |
| Maximum Volumetric Flow Rate |
55 mm³/s* |
| Maximum Temperature |
300 °C |
| Heat Break Material |
Titanium alloy |
| Internal Heat Break Surface Roughness |
Ra ≤ 0.2 μm (typical) |
| Dimensions |
48 × 26.5 × 15 mm |
| Weight |
24 g |
| Package Variant |
1-Pack (1 hotend) |
* The maximum volumetric flow rate and comparative performance figures are based on manufacturer testing. Actual results depend on printing conditions.
Package Contents
Liber™ High Flow Hotend with a 0.4 mm nozzle and thermistor — 1 pc.; M3×12 mounting screws — 2 pcs. Informational materials may also be included in the factory packaging.
© Look-Feel-Live-3D (LFL3D). Copying this content without permission and proper attribution is prohibited.